


Tu prototipo está aprobado. Funciona. Se ve genial. Ahora viene la siguiente gran pregunta. ¿Cómo haces mil de ellos? ¿O diez mil? ¿O más?
Crear una sola pieza perfecta es un desafío. Recrear esa perfección miles de veces con una velocidad y consistencia increíbles es otro desafío completamente diferente. Este es el puente que debes cruzar desde la creación de prototipos hasta la producción.
Para crear piezas de plástico de alta calidad a escala, un proceso se destaca por encima de todos los demás. Es el estándar de oro de la fabricación. Es el motor de la producción en masa moderna. Ese proceso es Moldeo por Inyección.
Esta guía servirá como tu introducción completa a esta poderosa tecnología. Exploraremos el proceso, los materiales, las reglas de diseño y los costos. Es tu hoja de ruta para navegar con éxito el camino hacia la producción escalable.
Desglosando el proceso de moldeo por inyección
Un mundo de materiales para moldeo por inyección
Diseñando para el éxito (DFM)
Explorando técnicas avanzadas
Descifrando la estructura de costos
Perfeccionando el aspecto final: acabados superficiales
Asegurando la calidad, evitando defectos
Impulsando las principales industrias del mundo
Desglosando el proceso de moldeo por inyección
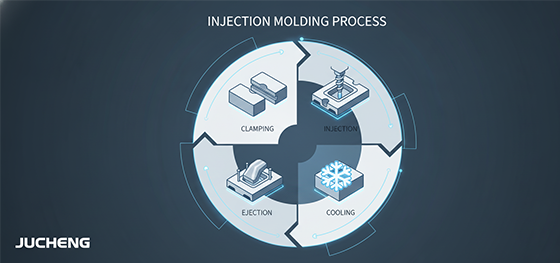
El proceso de moldeo por inyección is a high-speed cycle of creation. It is a highly controlled and repeatable dance of pressure, heat, and motion. The cycle includes mold closing, filling and packing, cooling, and ejection.
It begins with Clamping. The machine holds the mold closed against the pressure generated during filling and packing. Required clamp force depends on the projected area and cavity pressure, rather than a fixed tonnage range for every part.
Next is Injection and Packing. Plastic pellets are melted in the barrel and injected into the mold cavity. Filling time depends on the part, material, and process settings. Packing or holding pressure then feeds additional material into the cavity to compensate for cooling shrinkage while the gate remains open.
Cooling continues while the mold remains closed until the part is sufficiently solid for ejection. The material shrinks as it cools, so the final dimensions are not an exact copy of the cavity dimensions. Cooling is often the longest portion of the cycle.
Finalmente, la Expulsión. El molde se abre y un sistema de pasadores expulsores empuja la pieza ya sólida fuera del molde. La pieza cae en un contenedor de recolección y el ciclo comienza inmediatamente de nuevo.
Un mundo de materiales para moldeo por inyección
Una increíble variedad de termoplásticos Los materiales de moldeo por inyección puede ser utilizada. Elegir el correcto es una decisión de diseño crítica.
Los plásticos de uso general son los caballos de batalla. Materiales como el Polipropileno (PP) y el Polietileno (PE) son de muy bajo costo y se utilizan para bienes de consumo cotidianos, envases y juguetes.
Los plásticos de ingeniería ofrecen un nivel superior de rendimiento. El ABS, el Policarbonato (PC) y el Nailon (PA) proporcionan un gran equilibrio entre resistencia, resistencia al impacto y costo. Son la columna vertebral de piezas automotrices, carcasas electrónicas y bienes duraderos.
High-performance thermoplastics such as PEEK and PEI (ULTEM) can be considered for demanding applications, but their heat and chemical resistance are not interchangeable. Evaluate the specific grade against the operating temperature, load, chemicals, and exposure conditions. Aerospace or medical use requires assessment of the selected grade and finished part for the intended application, not just the polymer name.
Thermoplastic elastomers (TPEs), including thermoplastic polyurethane (TPU), cover a range of hardness and performance characteristics. Selected grades can be used for grips, seals, and overmolded parts; suitability depends on the specific formulation, operating temperature, fluid exposure, and mechanical requirements. For overmolding, substrate compatibility and bond performance also need evaluation. At JUCHENG, we stock over 50 common resins and can help you select the perfect material.
Diseñando para el éxito (DFM)
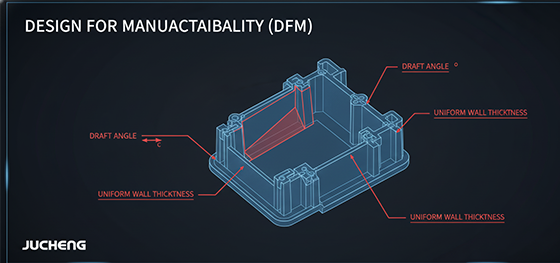
No se puede simplemente tomar un diseño hecho para impresión 3D e inyectarlo. Una pieza debe estar diseñada específicamente para el proceso de moldeo. Esto se llama Diseño para Fabricabilidad, o DFM.
Un diseño de moldeo por inyección is a deep topic. But two rules are the most important. First, maintain a uniform wall thickness. Thick sections cool slower than thin sections, which can cause ugly sink marks and warping. Second, assess draft relative to the intended pull direction, taking the material, surface texture, and feature depth into account. Draft helps surfaces release from the mold. Intentional undercuts, such as snap-fit features, need an appropriate tooling and release strategy rather than a blanket draft rule.
Comprender el DFM es crítico para el éxito. En JUCHENG, nuestra Revisión de DFM Gratuita es una parte central de nuestro servicio. Nuestros ingenieros analizan su diseño y brindan comentarios expertos para prevenir problemas antes de que ocurran.
Explorando técnicas avanzadas

El moldeo moderno es capaz de una complejidad increíble. El debate de sobremoldeo vs moldeo por inserción showcases two powerful techniques.
Insert molding places a preformed component into the mold before plastic injection. For a threaded metal insert, plastic surrounds the external body to retain it while the internal thread remains accessible for a screw. Molded-in inserts are one option; heat or ultrasonic installation into thermoplastics and other post-mold methods may also be suitable. Choose the insert and installation method for the plastic, joint loads, and assembly requirements.
Overmolding adds a molded material over a substrate. In pick-and-place molding, previously molded substrate parts are placed into a separate overmold tool. Two-shot molding instead forms and overmolds the substrate in an integrated sequence, using approaches such as transfer, rotation, or core-back tooling. A soft TPE grip over a rigid substrate is one application, not the only material combination. Material compatibility and processing conditions must be evaluated for the intended bond.
Descifrando la estructura de costos
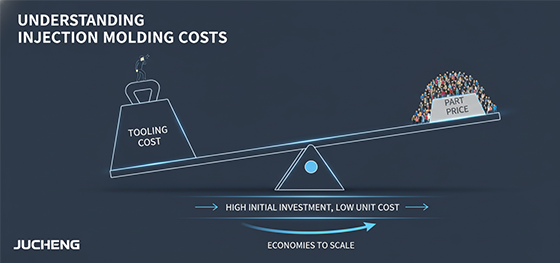
Understanding the costo de moldeo por inyección is key to planning your project. It is a story of two numbers: the mold cost and the part price.
Tooling is an upfront project cost. Injection molds may use aluminum or steel; tooling cost depends on the part size and complexity, mold material, cavity count, and required finish.
Per-part cost depends on material consumption, machine time, cycle time, and the number of parts produced per cycle. Increasing production quantity spreads the upfront tooling cost across more parts, but does not guarantee a particular unit price or make molding the lowest-cost option for every project. Compare total project costs at the required quantity. For smaller volumes, JUCHENG offers low-volume tooling options that lower your upfront investment.
Perfeccionando el aspecto final: acabados superficiales
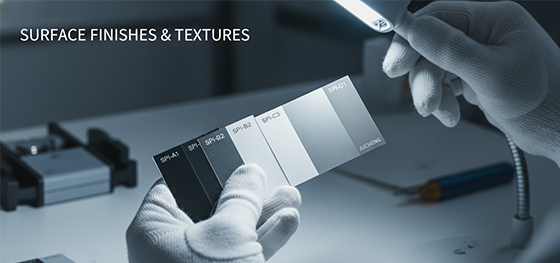
The mold surface influences the molded finish, but the selected resin and additives can affect how the texture appears on the part. This means we can achieve a huge variety of Acabados superficiales en moldeo por inyección by treating the steel mold itself.
The industry uses SPI (Society of the Plastics Industry) standards to define these finishes. SPI-A1 specifies a diamond-polished mold finish associated with high gloss, while B-grade finishes use abrasive paper. C and D finishes use different methods: SPI-C1 uses a 600-grit stone, whereas SPI-D1 uses dry blasting. The molded appearance should be checked with the selected material rather than assumed from the finish designation alone.
We can also create complex patterns. VDI 3400 provides a reference for specifying EDM surface-texture grades; it is not the machining operation itself. Electrical discharge machining (EDM), also called spark erosion, can produce the mold texture. Other custom textures, like a leather grain, can also be chemically etched into the mold. This allows you to create beautiful, finished parts directly from the machine.
Asegurando la calidad, evitando defectos

A fast process is useless without quality. A professional manufacturer has a robust system to prevent Injection molding defects.
Defects such as sink marks and warping can result from interacting part-design, material, mold, and process factors. DFM can identify risks early, but proposed changes still need evaluation through molding trials and part inspection.
Flash and short shots also require assessment of the part geometry, mold design and condition, material, and process settings. Our experienced engineers use advanced tools like Moldflow simulation to predict how the plastic will flow. Simulation helps identify flow risks and compare design options; its predictions depend on the input data and modeling assumptions and must be checked against molding trials. During production, we use a data-driven "scientific molding" approach. Monitoring pressure, temperature, and time can help detect process variation, but monitoring alone does not establish that every part meets its requirements. Process validation and the applicable part inspections and acceptance criteria remain necessary. Finally, our QA department uses CMMs and other tools to verify that the final parts meet every one of your specifications.
Impulsando las principales industrias del mundo

El aplicaciones de moldeo por inyección are virtually endless. If a product is made of plastic and produced in high volume, it was likely injection molded.
In the Automotive industry, we produce parts that must meet the strict IATF 16949 quality standard. In the Medical field, we operate under ISO 13485 to create device components from biocompatible materials. For Consumer Electronics, we excel at producing the thin-walled, beautiful enclosures that define modern products.
Holding these key certifications is not just a formality. It is proof that we have the processes, traceability, and quality mindset to serve the world's most demanding industries. It is your assurance that we are a partner you can trust.
Choosing to invest in injection molding is a major step. It is the step that takes your product from a prototype to a real, scalable product. At JUCHENG, we specialize in helping companies make this transition, especially for low-volume production. We are your expert partner on the journey to market success.

