


Lidiar con cobre puro en un entorno aditivo se siente como intentar derretir un espejo con una linterna. En la jerarquía tradicional de la impresión 3D de metales, el cobre es el rebelde definitivo. Mientras que el titanio y el acero cooperan con los láseres infrarrojos estándar, el cobre refleja casi el 95% de esa energía, haciendo que el láser rebote inofensivamente—o peligrosamente—fuera del lecho de polvo. Esta resistencia física se ve agravada por la legendaria conductividad térmica del material. Incluso cuando logras provocar una fusión, el cobre circundante extrae ese calor tan rápidamente que el charco líquido se congela prematuramente, resultando en "castillos de arena" porosos y frágiles en lugar de componentes de ingeniería sólidos. Esta es la realidad de alto riesgo de la impresión 3D de cobre. Es un proceso donde el fabricante debe superar las leyes fundamentales de la termodinámica para lograr la densidad del 99.9% requerida para aplicaciones de alto voltaje y alta temperatura.
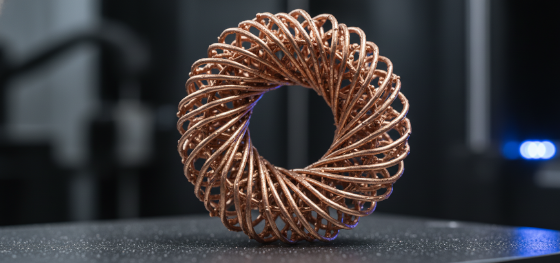
Jucheng Precision ha descartado el enfoque "estándar" para la fabricación aditiva de metales para esta aleación específica. Reconocemos que para una bobina de inducción o una placa fría de vehículo eléctrico, no hay margen para el compromiso en el rendimiento eléctrico o térmico. Si el cobre no es puro, o si la densidad es baja, la pieza se sobrecalentará y fallará bajo carga. Nuestra instalación ha entrado en la era de "longitud de onda corta", utilizando sistemas láser avanzados y oscilación de haz especializada para cerrar la brecha entre la ciencia de los materiales de impresión 3D y la realidad funcional. Esta guía ignora las definiciones superficiales para sumergirse en la microfísica de la absorción del láser verde, la lucha por el control de oxígeno en la cámara, y por qué nuestro procesamiento posterior integrado asegura que sus diseños de cobre funcionen con la misma integridad cristalina que un tocho forjado en bruto.
La precisión en el crecimiento del cobre es una lucha contra la pérdida inmediata de calor. No solo estás sinterizando polvo; estás gestionando un evento violento de cambio de fase a alta velocidad que se niega a permanecer localizado. Ya sea que estés construyendo un intercambiador de calor subminiatura para un satélite o una barra colectora compleja para un inversor de alto rendimiento, la lógica de la absorción es tu principal gobernador de ingeniería. Examinemos los pilares técnicos de la fabricación aditiva de cobre de alta pureza y veamos cómo nuestra instalación fija la integridad de tus diseños más conductivos en la realidad física.
Crisis de Reflectividad: Por Qué los Láseres Infrarrojos Rebotan
Trampa de Sumidero Térmico: Gestión del Charco de Fusión en Tiempo Real
Inducción y Refrigeración de VE: Aplicaciones de Alta Conductividad
Pureza del Material: Asegurando un Rendimiento IACS del 99.9%
Hybrid Integration: Why 5-Axis CNC and DMLS Must Coexist
Crisis de Reflectividad: Por Qué los Láseres Infrarrojos Rebotan

Para dominar impresión 3D de cobre, you must first acknowledge the failure of the 1064nm wavelength. Most metal 3D printers utilize fiber lasers in the near-infrared spectrum. For titanium or steel, these lasers are efficient "slicers." For copper, they are essentially laser pointers. At room temperature, copper absorbs less than 5% of infrared light. The rest of the energy is scattered, which can damage the machine's optics and prevents the powder from reaching its melting point. This is the "Reflectivity Crisis" that kept pure copper in the experimental category for years.
The engineering solution involves a shift in the electromagnetic spectrum. Jucheng Precision leverages high-power Green Lasers (515nm wavelength) to overcome this barrier. Copper absorbs green light roughly eight times more efficiently than infrared. This allows us to achieve a stable melt pool with much lower power requirements, ensuring that we are welding the particles rather than just blasting them. Another strategy involves using ultra-high-power infrared lasers (up to 1kW) with a "pre-heat" pass to lower the reflectivity of the material before the final fusion. By managing the optical encounter between the photon and the copper atom, we ensure that the energy stays where it belongs: in the part. This optical control is the first pillar of industrial-grade copper production, enabling the creation of dense, complex features that were once considered the exclusive domain of traditional casting or high-risk brazing.
Trampa de Sumidero Térmico: Gestión del Charco de Fusión en Tiempo Real
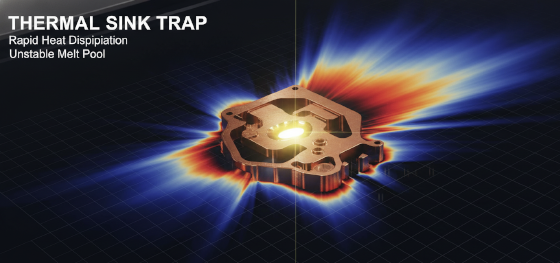
If the laser is the hammer, the material's thermal conductivity is a massive sponge. Copper conducts heat at approximately 400 W/m-K—about 40 times faster than titanium. As the laser moves, the copper substrate acts as a heat sink, drawing the thermal energy away from the melt pool almost as fast as the laser can provide it. This leads to "balling"—a defect where the molten metal forms into isolated spheres instead of a continuous weld bead. It is a constant battle to keep the liquid "wet" enough to bond with the previous layer.
Our solution involves a sophisticated "Heat Management Toolpath." We don't just scan in straight lines; we utilize beam oscillation (wobble) and high-frequency pulse control to keep the melt pool active longer. This technique allows us to achieve a theoretical density exceeding 99.7%, which is vital for pressure-tight fluid applications. We also pay close attention to the build plate temperature. By maintaining a high-temperature pre-heat on the substrate, we reduce the "Thermal Shock" experienced by the first several hundred layers. This thermal sovereignty ensures that internal stresses don't build up to the point of cracking or delamination. In a material that naturally wants to shed heat, our process forces the energy to stay concentrated, building the structural soul of your design with a level of density that defies the material's own physical urges.
Inducción y Refrigeración de VE: Aplicaciones de Alta Conductividad

Why go through the immense difficulty of copper additive? Because certain modern designs have outgrown the drill bit. In the world of Electric Vehicles (EVs), thermal density is skyrocketing. We are asked to pack 100kW of power into inverter housings the size of a lunchbox. These systems require complex, monolithic "Cold Plates" with internal cooling channels that follow the exact path of the heat-generating semiconductors. Copper 3d printing is the only way to realize these "Internal Labyrinths."
Another vital frontier is the manufacturing of Induction Coils. Traditional coils are hand-bent from copper tubing, which limits them to simple shapes and inconsistent performance. With 3D printing, we can produce coils with square or elliptical cross-sections and integrated internal cooling vents that are mathematically optimized for the electromagnetic field they generate. These "perfect" coils increase the efficiency of industrial heat-treatment lines by up to 20%. We also serve the high-frequency electronics sector, producing busbars and RF heat sinks that combine the light-weighting potential of lattice structures with the raw electrical performance of pure copper. By removing the geometric shackles of the machine shop, we empower our clients to design for the peak of electrical and thermal physics.
Pureza del Material: Asegurando un Rendimiento IACS del 99.9%

For a copper part, "close enough" in material purity is a failure. If the copper powder contains even minor amounts of oxygen or iron, the electrical conductivity—measured in % IACS (International Annealed Copper Standard)—will plummet. A part that looks like copper but only has 70% IACS is essentially a giant resistor that will melt itself under high current. Jucheng Precision operates a "Purity First" supply chain. We utilize high-purity, gas-atomized spherical copper powder with a median particle size optimized for thin-layer flow.
We verify our results through rigorous four-point probe testing and eddy-current conductivity audits. Our 3D printed copper components routinely achieve 100% to 102% IACS after a stabilized vacuum-annealing cycle. This thermal stabilization is mandatory; it allows the copper grains to grow and reorganize, removing the boundaries that impede electron flow. We treat the metallurgical data with the same technical reverence as the dimensional tolerances. When you receive a busbar or an electrode from JUCHENG, you aren't just getting a copper shape; you are getting a verified conduit for high-energy physics, backed by a paper trail that proves its crystalline integrity.
Hybrid Integration: Why 5-Axis CNC and DMLS Must Coexist
The final hallmark of a world-class copper facility is the ability to close the loop on accuracy. A raw 3D print in copper has a surface finish that is too rough for a high-pressure seal or a precision electrical contact. This is the "Accuracy Gap" that Jucheng Precision eliminates through our hybrid manufacturing ecosystem. We utilize our in-house 5-axis CNC machines to perform the final "surgical strike" on your printed copper parts.
Because copper is gummy and difficult to mill, we utilize the same high-speed, diamond-polished tooling that we use in our Custom Metal Parts department. We can finish a 3D-printed internal bore to a +/- 0.01mm tolerance and an Ra 0.4 µm finish. This integration of additive and subtractive means you don't have to choose between complexity and precision—you get both. We manage the entire lifecycle, from the initial XRF material verification to the final CMM dimensional audit. Whether you are building the next generation of EV charging hardware or a high-efficiency aerospace radiator, our expertise in copper additive and 5-axis finishing ensures your vision is delivered with absolute structural and electrical integrity. Contact our team today for a technical DFM review and see how our copper protocols can armor your next high-energy breakthrough.

